
Home > CaseCircular vibrating screenConveyor equipmentEnvironmentally friendly vibrating screenFAQfeeding equipmentGroup NewsIndustry NewsLinear vibrating screenNewsProduct KnowledgeProductsServiceSpare parts categoryVideo未分类暂停使用 > ZGS Heavy-Duty Vibrating Screen – Principle and Structure
China has currently produced the ZGS series self-synchronous probabilistic screens. This type of screen operates on the principle of two vibrating motors rotating in opposite directions; the unbalanced force (inertial force) generated by the eccentric masses at both ends of the motors drives the screen machine to undergo reciprocating vibration in a specific direction. When the two vibrating motors rotate synchronously and in opposite directions, the excitation forces produced by their eccentric masses cancel each other out in the direction parallel to the motor axes, while their resultant force in the direction perpendicular to the motor axes combines to form a net force. As a result, the motion trajectory of the screen machine is a straight line. The relative surfaces of the two motor shafts are inclined at an angle in the vertical direction; under the combined action of this excitation force and the gravitational force of the material, the material is thrown upward, jumps, or moves forward in a straight line along the surface, thereby achieving the purpose of screening and grading the material.
Since the vibrating motor is directly fixed to the screen machine’s frame without any elastic connection in between, it forms a single-particle forced vibration system; as the screen machine operates outside the resonance range, it remains insensitive to load variations, ensuring smooth operation. The unbalanced forces generated add up and cancel out, causing the screen machine to undergo linear reciprocating motion, thereby defining its linear vibration trajectory. When material falls into the first layer of the screen from the inlet, large particles—whose size exceeds the aperture spacing of the first screen layer—are separated more efficiently under the vibration of the screen surface; the remaining small-and medium-sized particles are then further separated by the second and third screen layers by the same mechanism. The large particles from the first, second, and third screen layers simultaneously enter the coal crusher inlet for crushing, while the material passing through the third screen layer constitutes the qualified product, which is then fed into the next processing stage.
The probability screening system primarily consists of two main components: a vibration damping system and a screening unit.
(1) Shock Absorption System
The ZGS series self-synchronizing probability sieve features a hanging load-reducing system: the sieve body is suspended from a support frame using a rope clamp that connects a shock-absorbing spring, a cable helical fastener, and a steel wire rope; the spring serves to dampen vibrations.
(2) Sieving Unit
The screening unit consists of a screening box, a vibrating motor, and a screening surface.
III. Maintenance and Adjustment
(1) Lifting of the vibration damping system
Install the vibration damping system on the support frame as specified; suspend the screening machine using steel wire ropes and rope clamps; then adjust the adjustment screw to align the machine’s inlet horizontally and ensure that the four vibration damping springs are subjected to uniform force (this can be verified by measuring the compression height of each spring). If the compression heights are identical, the force distribution is uniform. A permissible tolerance may exist in the compression heights of the springs on the front and rear vibration dampers; however, the compression heights of the two springs in each set must be adjusted to be identical. When a spring requires replacement due to damage, the entire set of springs must be replaced simultaneously.
(2) Pre-installation Instructions for Sieve Plate Installation
(1) Amplitude adjustment requirements and methods
When the machine is running under no-load conditions, set the screen’s vibration amplitude to 4–5 mm; alternatively, adjust the amplitude appropriately based on the coal quality (for example, use a higher amplitude – generally not exceeding 6 mm – when the coal is dense or the processing volume is high; use a lower amplitude when the coal is loose or the processing volume is low). This approach extends the machine’s service life and reduces noise levels.
The method for adjusting the amplitude involves changing the eccentric coincidence angle between the two motors; however, the coincidence angles of the four sets of eccentric blocks on both motors must be made identical; otherwise, oscillation will occur. After the eccentric blocks have been properly adjusted, a locking nut should be tightened to set the amplitude to the desired value, and then a locking washer should be installed and secured. The amplitude can be directly read from the scale markings on the amplitude indicator plate—the value indicated by the horizontal coordinate of the intersection point of the two lines represents the adjusted amplitude.
The article data is sourced from 360 Wenku.

Strict inspection before the product leaves the factory; Organize shipment according to the contract.
Assign dedicated after-sales service personnel to the site to provide guidance
Installation, debugging, and trial operation of guiding equipment;
Problems encountered by domestic customers during the production process, service
The staff guarantee to provide clear instructions within 24 hours
The solution is to rush to the site for processing as quickly as possible.
Adequate equipment spare parts and timely supply of spare parts enable Users can rest assured.
Provide customers with first-class equipment, technology, and services
Give clear solutions
Safe, high-quality, and reliable
Crafty manufacturing, striving for excellence
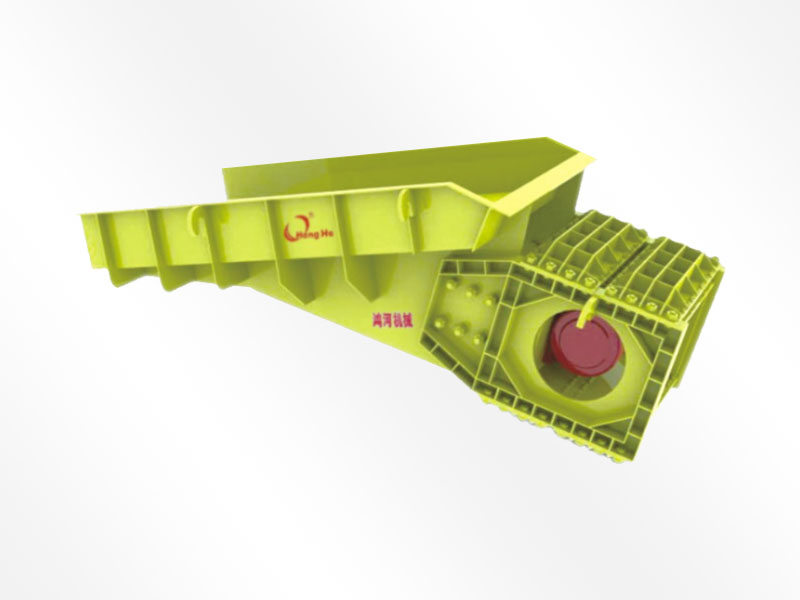 Double body vibrating feeder
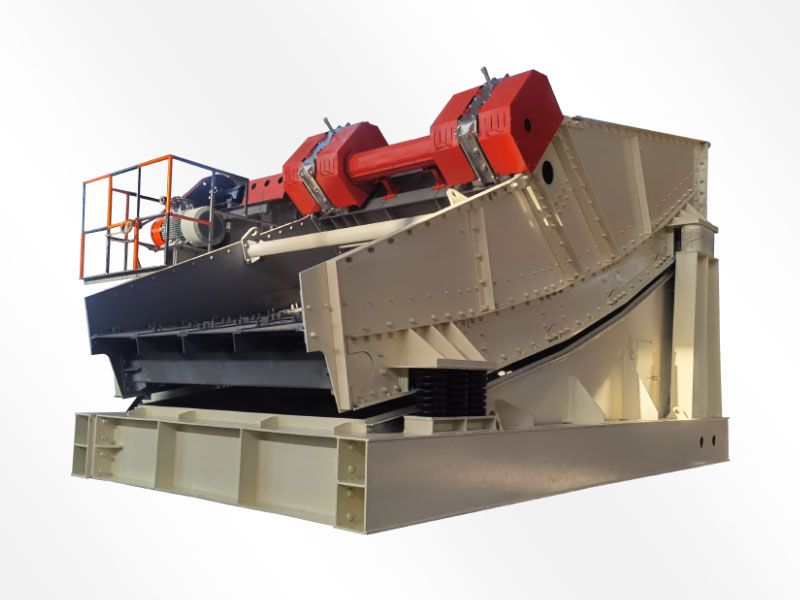 Banana shaped linear sieve
 Ceramic rod sieve plate

Email:
honghekj88@163.com
 0086-0373-5579588

 Spare Parts
 EN
